

Material Selection and Pretreatment
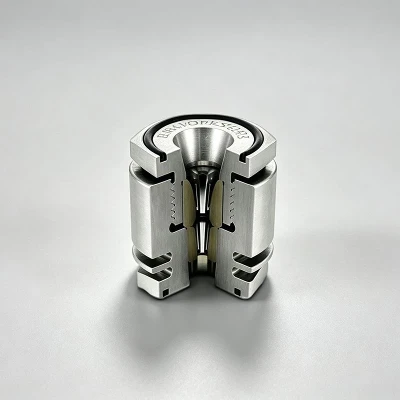
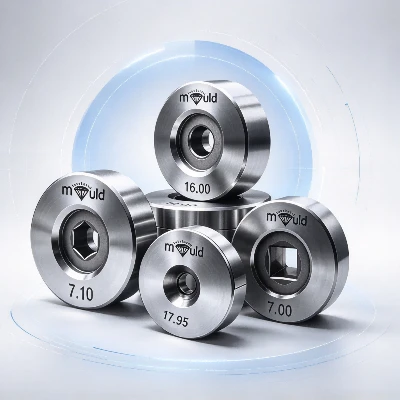
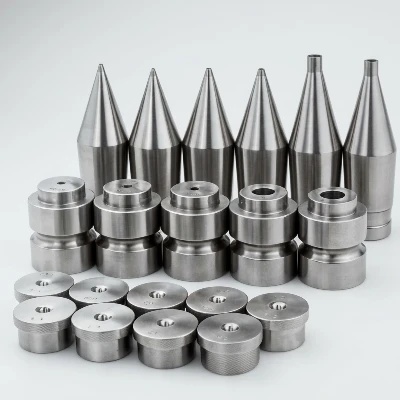
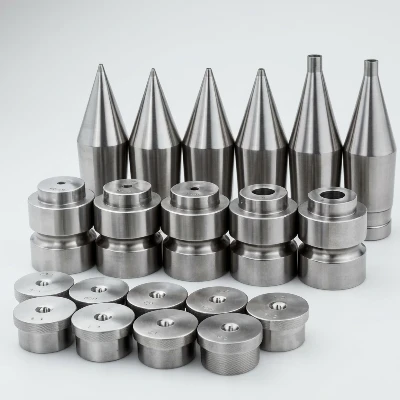
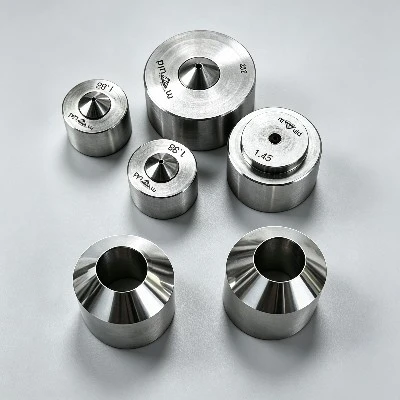
Die Steel: H13 hot work die steel (hardness HRC48-52) is preferred, as its high-temperature resistance and wear resistance are suitable for wire drawing processes. Referring to the *Die Engineering Handbook* (5th Edition), this material maintains stability even at 600℃.
Surface Treatment: Nitriding is recommended, achieving a surface hardness of HV1000 or higher, extending die life.
Temperature and Speed Control
Preheating Temperature: The die needs to be preheated to 200-300℃ (adjusted according to material thickness) to avoid cracking caused by cold drawing.
Drawing Speed: 0.5-1.2 m/min is recommended for irregularly shaped dies; for complex shapes, the speed should be reduced to below 0.3 m/min to ensure uniform wire deformation.
Lubricant Selection
High-viscosity lubricants (such as graphite-containing oil-based lubricants) can reduce friction and lower die wear rate by approximately 30% (Source: *Metal Forming Technology*).